close
Choose Your Site
Global
Social Media





| Quantity: | |
|---|---|


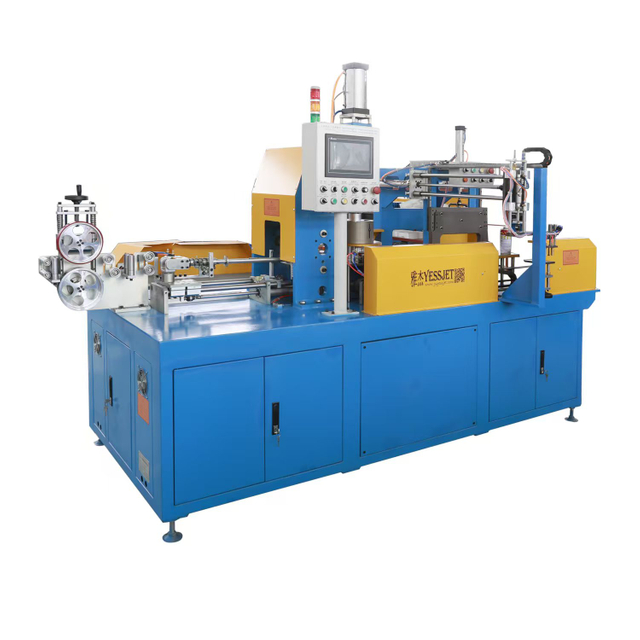
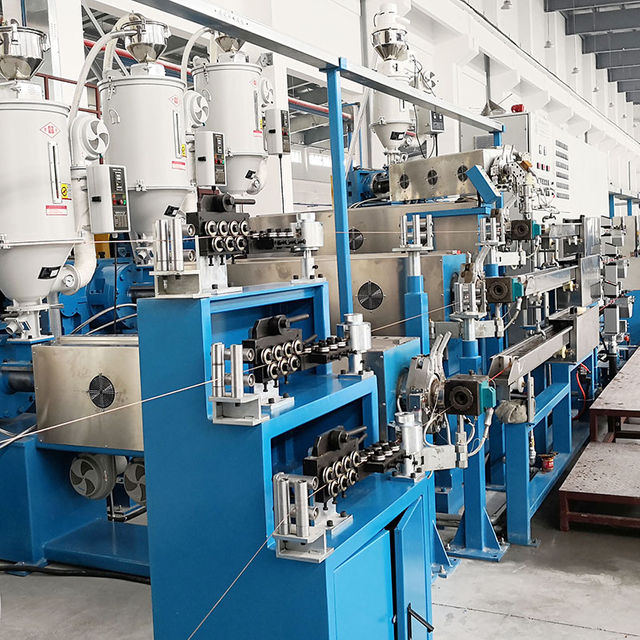
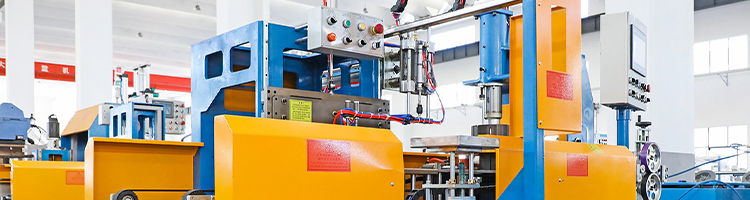
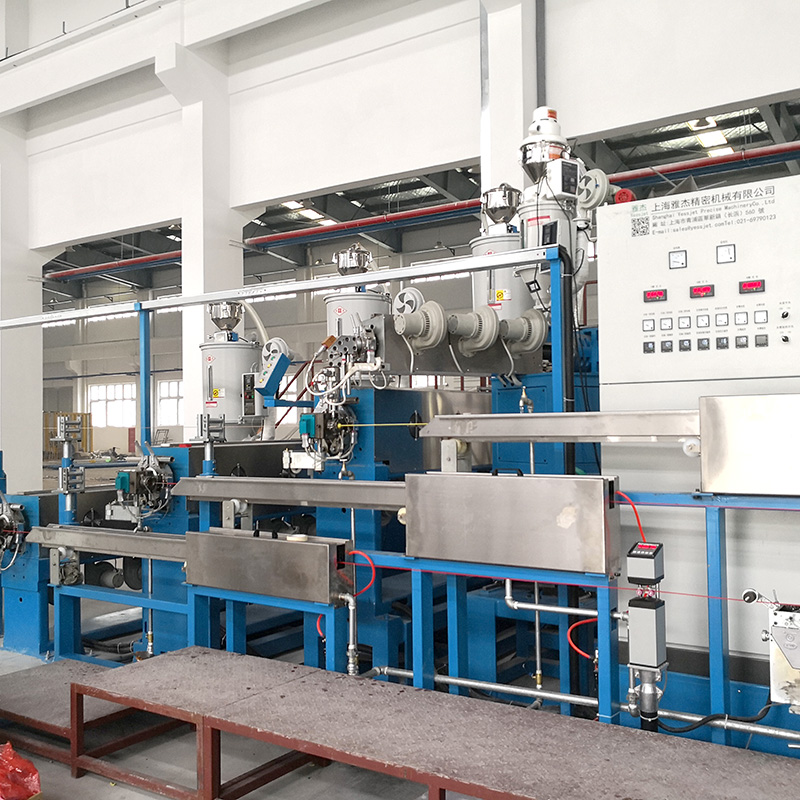
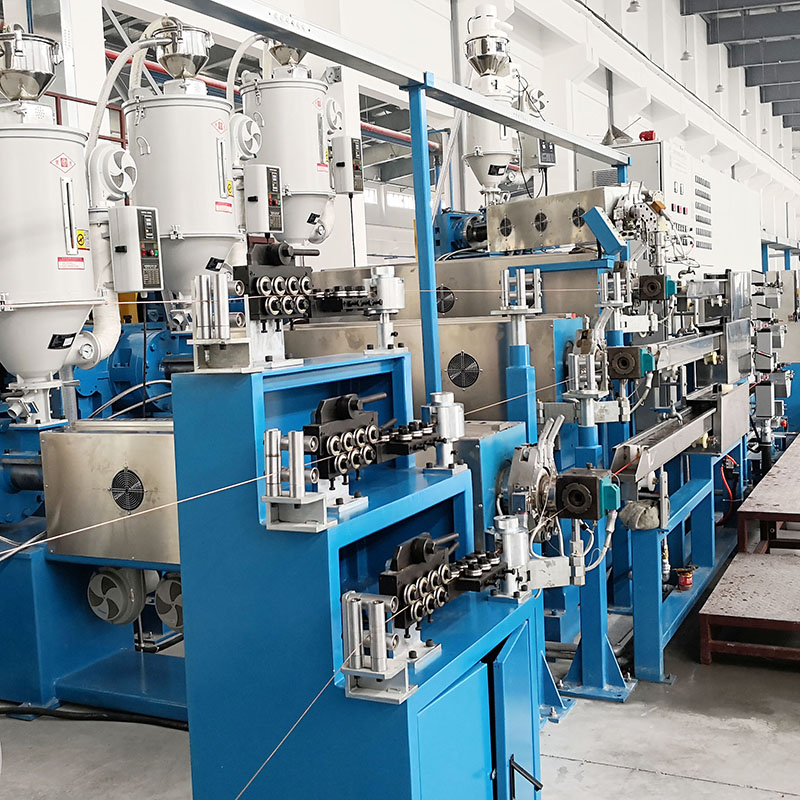
This LSZH cable extruder is engineered for commercial cable manufacturers producing low-smoke zero-halogen wire and cable products. It integrates a material preheating system, low-shear extrusion structure and precision die head to address common processing challenges of LSZH compounds, including poor flowability, temperature sensitivity and moisture absorption. The equipment supports continuous production of LSZH cables, with insulation thickness tolerance controlled within ±0.02mm.
The machine is fitted with a stainless steel preheater hopper with 150kg capacity, adopting hot-air circulation technology to maintain material temperature at 80-100℃ with ±2℃ accuracy. This pre-conditioning process softens LSZH granules and removes absorbed moisture (which can reach up to 0.3% of material weight under ambient storage). Compared with unheated processing setups, this system reduces extrusion torque by 25% and eliminates cold spots in the melted compound. The upper temperature limit is set below 120℃ to avoid material caking inside the hopper.
A dual-screw feeding unit with 1.5kW power is installed at the feeding inlet, providing enhanced mixing capability for LSZH compounds. This structure promotes uniform dispersion of flame-retardant additives in the material matrix, reducing insulation defects such as pinholes and uneven hardness. The feeding unit operates in sync with the main extruder to maintain consistent material supply speed across production cycles.
The main extruder adopts an SJ45 model screw with a 33:1 length-to-diameter (L/D) ratio and low-shear profile. This design protects the molecular structure of LSZH compounds during extrusion, a key factor for retaining the material’s flame-retardant properties after processing. The system includes 5 independent temperature control zones with total heating power of 7.5kW. The metering zone is fitted with water cooling to stabilize processing temperature within 170-200℃, the standard processing range for LSZH compounds.
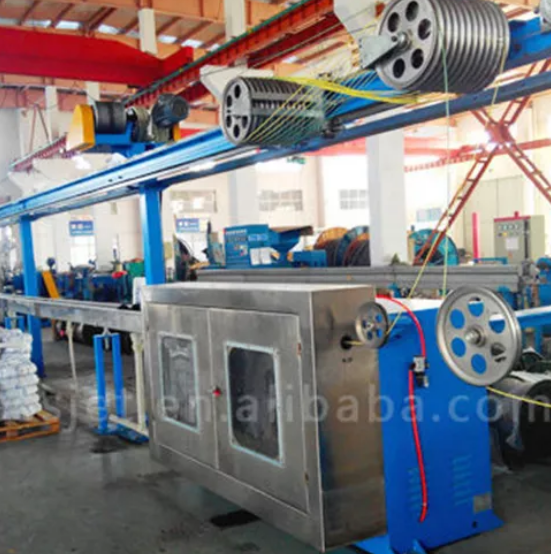
A 3-section vacuum cooling tank with 3000mm length is configured after the extrusion die head. This cooling system reduces cable surface temperature from 200℃ to 40℃ within 12 seconds, supporting continuous high-speed production while stabilizing insulation layer dimensions. The vacuum structure ensures even cooling around the cable circumference, avoiding ovality or thickness deviation caused by uneven temperature distribution.
Parameter Category | Specific Indicator | Value |
|---|---|---|
Preheater System | Hopper capacity | 150kg |
Operating temperature range | 80-100℃ | |
Temperature control accuracy | ±2℃ | |
Feeding Unit | Structure | Dual-screw |
Rated power | 1.5kW | |
Main Extruder | Screw model | SJ45 |
L/D ratio | 33:1 | |
Temperature control zones | 5 zones | |
Total heating power | 7.5kW | |
Processing temperature range | 170-200℃ | |
Cooling System | Tank structure | 3-section vacuum |
Total tank length | 3000mm | |
Cooling cycle (200℃ to 40℃) | 12 seconds | |
Precision Performance | Insulation thickness tolerance | ±0.02mm |
The equipment adopts a Siemens PLC control system paired with a 7-inch HMI touchscreen. The system can store up to 25 material-specific parameter profiles, including settings for polyolefin-based and elastomer-based LSZH compounds, allowing operators to recall corresponding parameters with one click during product changeover. The system also reserves interfaces for smoke density and halogen content testing devices, compatible with third-party detectors for production process verification.
LSZH granules absorb moisture easily under ambient storage conditions, with water content reaching up to 0.3%. Trapped moisture will form bubbles inside the insulation layer during high-temperature extrusion, leading to insulation performance defects. The preheater removes absorbed moisture and softens granules before extrusion, reducing product defect rates by 40% compared with non-preheated processing.
Yes, the equipment can process recycled LSZH materials, with recycled content not exceeding 30% of total material volume. The preheater and dual-screw mixing system homogenize recycled and virgin materials to maintain consistent extrusion performance and finished product properties.
Clean the interior of the preheater hopper every 48 hours of operation, and calibrate the temperature sensor on a monthly basis. Material caking occurs when processing temperature exceeds 120℃ for LSZH compounds, so regular calibration is required to ensure control accuracy.
Cables produced with this equipment comply with EN 50267-2-1 (low smoke zero halogen requirements) and EN 60332-1-2 (flame spread specifications). Corresponding test reports can be provided upon request for compliance verification.